Specifying valves for a power plant is unforgiving. When saturated or superheated steam pushes past 400°C, the rules that work for water and air no longer apply—pressure ratings fall, carbon steel creeps, and a packing gland fine at 200°C starts to weep. If you run a boiler, turbine, or auxiliary steam system, a wrong choice means forced outages and emergency replacements. In this guide we show how high temperature reshapes valve selection, the materials and structures that survive it, and how gate valves and globe valves earn their place in your plant.
Not sure which valve your line needs?
Our application engineers will review your P&ID, media, and operating window and recommend the right specification—free of charge.
The first mistake you can make is treating a high-temperature valve as a standard valve that simply runs hotter. It is not. Three things happen to a valve as temperature climbs, and each one directly changes what you should buy.
Pressure–temperature derating. A valve’s allowable working pressure is not fixed—it drops as temperature rises. The same Class 300 body that handles 51 bar at 38°C may be limited to a fraction of that at 540°C. You must read the ASME B16.34 rating curve for your exact temperature, not the nameplate class alone.
Creep and loss of strength. Above roughly 400°C, carbon steel begins to creep: it slowly deforms under load even below its yield point. Bolting loosens, seats distort, and a valve that was tight at startup leaks after a few months of operation.
Thermal cycling and binding. Steam systems heat and cool repeatedly. Different metals expand at different rates, so a stem and bonnet that fit cold can bind hot. You need a design that tolerates that movement—and a seal that does not fail when the gland warms.
Full-Think tip: Never size a high-temperature valve from its cold pressure class. Pull the ASME B16.34 curve for your peak metal temperature, then add margin—most plants specify for the design temperature, not the operating average.
Material selection is where most high-temperature valve failures are decided. Your goal is a body that holds strength at temperature, a trim that resists erosion and galling, and a seal that does not soften or oxidize.
| Service temperature | Body material | Typical grades | Notes |
|---|---|---|---|
| Up to ~425°C | Carbon steel | WCB, WCC | Economical; limit near the creep threshold |
| 425–550°C | Low-alloy steel | WC6, WC9, C12A | The workhorse for main steam |
| 550–650°C | Stainless steel | CF8C (347), CF3M, 310/310S | Resists oxidation and creep |
| Above 650°C | Specialty alloy | Verify per project | Strict creep limits; confirm early |
For the trim—seats, disc, and stem—you want hardness and galling resistance. A 13Cr stem with Stellite® 6 hardfacing on seats is a common, proven choice for steam. When corrosion is also a factor (e.g., condensate with oxygen), you move toward stainless and duplex grades. If you are weighing cast versus forged bodies for thick-wall, high-pressure steam, our guide on cast steel vs forged steel valves breaks down where each wins, and our API 603 vs API 600 gate valve comparison explains stainless versus carbon steel gate construction.
Material is only half the story. The valve’s mechanical structure must manage pressure, temperature, and movement at the same time.
For low and medium classes, a bolted bonnet with a spiral-wound gasket is perfectly adequate. But on high-pressure steam lines (Class 600 and above), the pressure itself becomes your ally: a pressure-seal bonnet uses line pressure to tighten the seal as pressure rises, so it stays leak-tight where a bolted joint would need ever-tighter clamping. If your main steam or header is high class, specify pressure-seal.
Packing glands are the most common leak path on a hot valve. A bellows seal replaces the packed gland with a welded metal bellows, giving you a near-zero-emission stem—exactly what modern plants want for steam and thermal oil. Packing is still common and serviceable, but for throttling globe valves in steam duty, bellows sealing is the safer long-term choice. Our bellows seal vs packing seal guide covers the trade-offs in detail.
This is where material knowledge turns into a purchase order. Different valve types solve different power-plant problems, and the right choice depends on the duty, not the catalog.
A gate valve gives you a full-bore, low-pressure-drop path that is either fully open or fully closed—ideal for isolating main steam headers, turbine bypass, and boiler feed lines. For high-pressure steam, specify forged low-alloy bodies with a pressure-seal bonnet. You get a straight, unobstructed bore that pigs and cleans easily.
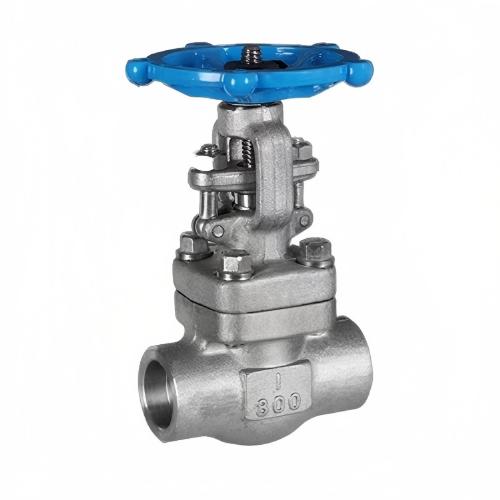
Browse our full range of high-temperature gate valves built to API 600, API 602, and API 603.
When you need to regulate flow—desuperheater water, gland steam, feedwater control—a globe valve is the right tool because its seat geometry throttles smoothly. In steam duty, choose a bellows-sealed globe valve in low-alloy or stainless steel so the stem stays emission-free through thousands of cycles.
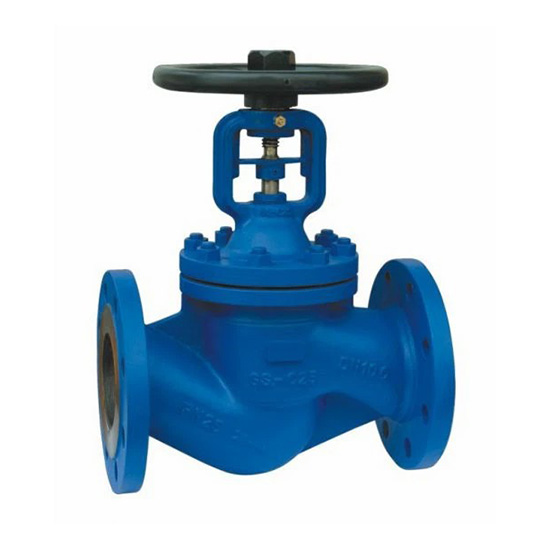
See our bellows-sealed globe valves to BS 1873 and API 603 for steam and boiler service.
Check valves protect pumps and turbines from reverse flow—critical on boiler feed and condensate lines. Swing, dual-plate, and pressure-seal check valves all have a place; dual-plate designs are compact and fast-closing, while pressure-seal checks suit the highest-class steam. Match the body material to the line so the check valve ages the same way as its neighbors. Explore our check valve range to BS 1868, API 594, and API 6D.
Browse our high-temperature valve range
From forged gate valves to bellows-sealed globe and pressure-seal check valves, we manufacture to API, ASME, BS/EN, and DIN standards—with full material traceability on every order.
When you sit down to specify, work the list in this order so nothing gets missed:
1. Define the duty. Peak metal temperature, design pressure, fluid state (saturated vs superheated steam), and whether the valve isolates, throttles, or protects against backflow.
2. Pick the material class. Use the temperature bands above and confirm against the ASME B16.34 rating for your exact temperature, not the nameplate class.
3. Choose the structure. Pressure-seal bonnet for Class 600+ steam; bellows seal for throttling stems; correct bolting and spiral-wound gaskets for the temperature.
4. Select the valve type. Gate for isolation, globe for regulation, check for backflow—linking the duty to the product, not the price list.
5. Anchor to standards. API 600/602/603 (gate), BS 1873 (globe), BS 1868/API 594 (check), API 6D (pipeline), and ASME B31.1 for power piping.
6. Demand traceability. Require mill test reports, heat numbers, and third-party inspection where the project calls for it—this is where low-cost bids quietly fail audit.
Use this quick-reference matrix as a starting point. Read across your temperature and duty, then confirm the final specification with the ASME B16.34 curve and your plant standards.
| Temperature | Duty | Recommended valve | Material / structure |
|---|---|---|---|
| Up to 425°C | Isolation | Gate valve | Carbon steel, bolted bonnet |
| 425–550°C | Isolation | Gate valve | Low-alloy (WC6/WC9), pressure-seal |
| Above 550°C | Isolation | Gate valve | Stainless (CF8C/310), pressure-seal |
| Any | Throttling | Globe valve | Alloy/stainless, bellows seal |
| Any | Backflow | Check valve | Match line body; dual-plate or pressure-seal |
To keep your specification defensible, anchor it to recognized standards: ASME B16.34 (pressure–temperature ratings), API 600 / 602 / 603 (gate valves), BS 1873 (globe), BS 1868 / API 594 (check), API 6D (pipeline), ASME B31.1 (power piping), and NACE MR0175/ISO 15156 where sour service is possible. Specifying to these standards lets your QA team verify dimensions, testing, and traceability instead of trusting a catalog claim. Our API valve standards guide explains what each one means for procurement.
Ready to specify with confidence?
Send us your line size, pressure class, media, and temperature. We return a matched valve specification with full material traceability—free of charge.
A WCB/WCC carbon steel body is generally used up to about 425°C (800°F); beyond that, creep becomes the limiting factor. From 425–550°C you should move to low-alloy steel such as WC6 or WC9, and above 550°C to stainless grades like CF8C (347) or 310/310S. The exact cutoff also depends on design life and bolting, so confirm against the ASME B16.34 curve.
On Class 600 and above, a bolted bonnet joint must stay clamped tight as pressure and temperature cycle, and bolt relaxation at high temperature is a constant risk. A pressure-seal bonnet uses the line pressure itself to energize the seal, so it actually gets tighter as pressure rises. That makes it the standard choice for main steam and high-pressure headers where a gasket leak is expensive.
No. PTFE degrades well below steam temperatures, and elastomers are out of the question above ~200°C. For high-temperature steam you need metal-to-metal or reinforced graphite seats. Metal seats also handle the thermal cycling and solid-particle erosion that soft seats cannot survive, though they trade away the bubble-tight shutoff of a soft seat.
Hot steam lines grow significantly and push loads into the nearest rigid component—often the valve. You should coordinate valve siting with the piping stress analysis, use proper supports and expansion loops or joints, and avoid cantilevered valve weights on long levers. Specifying an extended or finned bonnet (to keep the gland cooler) and confirming allowable nozzle loads with the valve maker prevents premature gland failure.
Boiler feedwater and steam drain lines combine high pressure with thermal shock and flashing, so they are punishing on trim. A hardened-trim globe or straight-through globe valve is typical for feedwater regulation, while drain lines often use a robust gate or a specialty drain valve with Stellite® faces. Check valves on these lines should be fast-closing (dual-plate) to protect the feed pump from backflow surges.
Standard B7 studs relax at high temperature, so specify alloy bolting such as A193 B16 (with B8M nuts) for elevated service. For gaskets, spiral-wound construction with a graphite filler and a proper centering ring is the norm; the winding and filler must be rated for your peak temperature. Mismatched bolting and gaskets are a common, avoidable source of hot flanged-joint leaks.
There is no single interval—it follows your plant’s risk-based inspection plan and the valve’s criticality. High-energy steam isolation and feedwater valves are typically examined on each major outage (often every 1–3 years) for seat leakage, bonnet joint integrity, and trim wear. Keeping a history of each valve’s test results lets you move from fixed schedules to condition-based maintenance and avoid unnecessary removals.
Yes. ASME B31.1 (Power Piping) adds plant-specific demands on valve pressure–temperature ratings, hydrostatic test pressures, and examination levels that go beyond a generic process-valve spec. It also ties valve qualification to the piping design conditions and outage philosophy. If you are buying for a power plant, confirm the valve is procured and tested to B31.1, not just a generic industrial standard.
They can be, but with limits. High-performance butterfly valves handle moderate-temperature steam in large low-pressure lines, while metal-seated plug valves resist abrasion but are less common in main steam. For true high-pressure, high-temperature steam isolation and throttling, gate and globe valves remain the safer, better-supported choice—which is why they dominate boiler and turbine auxiliaries. Consider butterflies/plugs only where size or cost forces the trade-off.
Require full material traceability: mill test reports with heat numbers, chemical and mechanical certificates for body and trim, heat-treatment records, and a hydrostatic/air-test certificate to API 598. For critical lines, specify third-party inspection (e.g., SGS/TÜV) and a witnessed seat-leak and shell-test. A supplier who cannot produce heat-level traceability—not just a generic certificate—is a risk on high-energy steam service.
Full-Think Valve (FULL-THINK VALVE CO., LTD) is an ISO 9001-certified industrial valve manufacturer established in 2012. For over 14 years we have designed, manufactured, and supplied ball, gate, globe, check, plug, butterfly valves, and strainers to the oil & gas, petrochemical, power, and water-treatment industries worldwide. All products are built to ANSI, ASME, API, BS/EN, DIN/EN, GB, and GOST standards, with full material traceability, mill test reports, and third-party inspection available on request. Our engineers review your P&ID and operating window before you place an order—so the valve you receive is specified for your plant, not a catalog.
Specifying high-temperature valves for a power plant comes down to one discipline: let operating temperature and duty drive the material, structure, and valve type—in that order. Start from the ASME B16.34 curve at your real peak temperature, choose low-alloy or stainless bodies with pressure-seal bonnets and bellows seals where steam demands them, and match gate, globe, and check valves to isolation, throttling, and backflow. If you would rather not work through the rating tables alone, our engineers will review your line and return a specification with full traceability—built for your plant, not a catalog average.
(All images are sourced from the internet. In the event of any copyright infringement, please contact us and we will remove the content promptly.)