Choosing a valve end connection is a decision you make early in a project — and live with for the life of your piping system. Get it right, and you get leak-free joints, straightforward maintenance, and a lower installed cost. Get it wrong, and you face expensive rework, fugitive emissions, or a valve you cannot service without cutting the pipe. In this guide, you will compare the three main valve connection types — flanged, welded, and threaded — and see how experienced engineers choose between them on real projects.
A valve end connection is the machined surface at each end of the valve body that joins the valve to the pipe. It determines how the joint is sealed, how much load the joint can carry, and whether you can remove the valve later without disturbing the piping. The three most common valve connection types are flanged ends, which bolt to matching pipe flanges; welded ends, which are fused permanently into the pipe; and threaded ends, which screw into the pipe or fittings. Every other decision — body material, trim, actuation — sits on top of this one, so it pays to get the end style right before you request quotations.
A flanged end connection gives you a bolted, gasket-sealed joint between the valve and a matching pipe flange. Faces are typically raised face (RF) per ASME B16.5, or EN 1092-1 types B1/B2 for DIN/EN piping, which is what you will find on most industrial steel valves. Because the joint is mechanical, you can break it with standard tools — no cutting, no welding machines, no hot work permit.
The trade-offs are real: flanged ends carry the highest initial cost (flanges, gaskets, and studs all add material and machining), every gasket is an additional leak path that can relax or blow out, and large high-class flanges dominate the valve’s weight and footprint.
You will normally specify a flanged end connection when the valve must be removable — isolation valves on equipment ties, control valve manifolds, and anywhere the actuator or trim needs regular access. They are also the default for large-diameter lines, where producing a full-penetration field weld is impractical. If your line carries high-cycle or abrasive media, pair flanged ends with a valve built for the duty, such as our ball valves for isolation and control duties across Class 150 to 600.
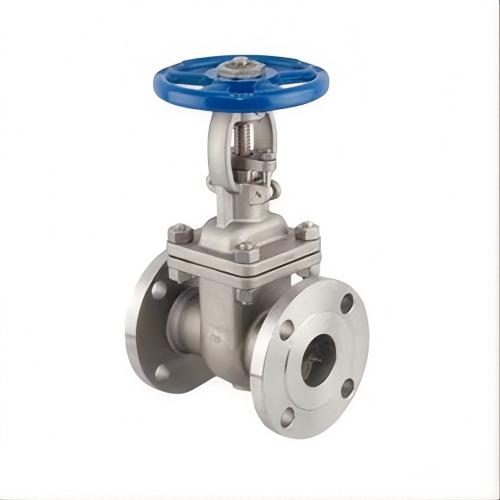
A flanged end gate valve: the raised-face flanges bolt to matching pipe flanges, so the valve can be unbolted for service.
Engineers often treat all welded valves as one category, but socket weld and butt weld are different joints with different rules, and choosing the wrong one creates rework at the pipe fabrication stage. Both give you a permanently sealed, gasket-free joint with the smallest leak path of any option — but they suit different pipe sizes, wall thicknesses, and inspection regimes.
A socket weld valve has machined sockets at each end: the pipe slides in, and a single fillet weld around the collar completes the joint. Dimensions follow ASME B16.11 in pressure classes 3000, 6000, and 9000, and the joint is intended for small-bore pipe — NPS 2 and smaller in most line classes. One fabrication detail you should enforce on site: leave a 1/16 in (1.6 mm) expansion gap between the pipe shoulder and the bottom of the socket before welding, or thermal expansion will load the fillet weld every cycle.
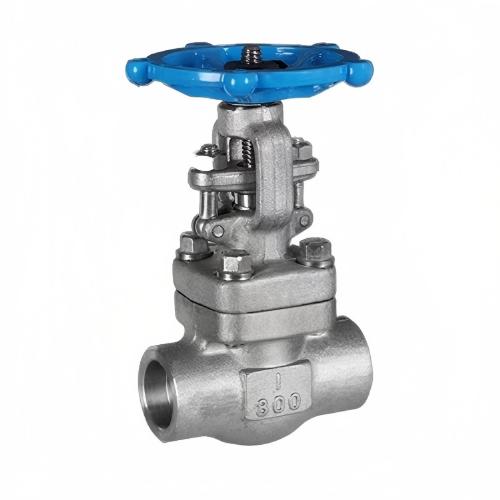
An API 602 forged steel gate valve with socket weld (SW) ends — the pipe slips into the machined sockets and is sealed with a fillet weld.
You will see socket weld valves on chemical injection lines, instrument takeoffs, and high-pressure small-bore header connections — anywhere the line is compact but the pressure is not. Most forged steel gate valves built to API 602 are ordered with SW ends for exactly this reason: the connection disappears into the pipe and the forged body keeps its pressure rating without oversized flanges.
A butt weld valve has bevelled ends prepared per ASME B16.25; the pipe and valve ends are butted together and joined with a full-penetration groove weld. The critical specification here is wall thickness: you must order the valve with the same schedule (Sch 40, 80, 160, and so on) as the pipe, so the weld transitions cleanly without a step in the flow path. Done correctly, a butt weld joint is effectively an extension of the pipe itself — smooth bore, no crevices, and fully radiographable.
Butt weld valves are the first choice for main process lines in power, LNG, and refinery service: high pressure and temperature, thermal cycling, and strict fugitive-emission targets all favor a fully welded joint. The trade-offs you accept are field welding with NDE on the weld (often RT or UT), and a valve that cannot be removed without cutting.
| Selection factor | Socket Weld (SW) | Butt Weld (BW) |
|---|---|---|
| Pipe size | NPS 2 and smaller | NPS 1/2 and larger; standard above NPS 2 |
| Joint design | Fillet weld into socket (ASME B16.11) | Full-penetration groove weld (ASME B16.25) |
| Pressure rating | Class 3000 / 6000 / 9000 | Any class; matches pipe schedule |
| Fatigue and thermal cycling | Crevice at the socket gap; poorer for cyclic duty | Smooth bore transition; best for cyclic service |
| Weld inspection | Visual and surface NDE only (fillet weld cannot be radiographed) | Fully radiographable (RT/UT) |
| Pipe schedule matching | Not required — the socket absorbs the bore step | Required — order the valve by pipe schedule |
As a rule of thumb, you will reach for a socket weld valve when the line is small-bore and fabrication happens in the shop, and a butt weld valve when the line is a main process header, the schedule is heavy, or the joint must be radiographed. If you want to settle the material side of the same decision, our guide on cast steel vs. forged steel valves pairs naturally with this one.
A threaded end valve screws directly into the pipe using NPT (ASME B1.20.1) or BSPT/BS 21 threads, so installation needs nothing more than a wrench and thread sealant. For a threaded end valve to stay tight, however, the joint depends on thread deformation — which makes it sensitive to vibration, thermal cycling, and repeated disassembly. In practice you will keep threaded ends to NPS 2 and smaller, at moderate pressures and temperatures.
When they make sense: instrument and sample lines, air and water utilities, skid-mounted piping, and other low-risk small-bore services where installation speed matters more than permanent integrity. In hydrocarbon plants, many operators permit threaded joints only below a pressure and temperature threshold, or require the threads to be seal-welded after tightening — check your company piping specification before you order. For demanding duties in the same small-bore envelope, a forged body such as our forged steel globe valves with SW ends usually costs little more and removes the joint-leak question entirely.
Rather than ranking the options in the abstract, run your application through six questions — this is how to choose valve end connections the way a piping engineer would on a real line:
| Criterion | Flanged (RF) | Socket Weld | Butt Weld | Threaded |
|---|---|---|---|---|
| Install speed | Moderate (bolt-up) | Fast | Slow (weld + NDE) | Fastest |
| Leak tightness | Good (gasket-dependent) | Very good | Best | Limited |
| Removability | Excellent | None (cut out) | None (cut out) | Good |
| Typical size range | NPS 1/2 – 48 | NPS 2 and smaller | NPS 1/2 – 48 and up | NPS 2 and smaller |
| Best fit | Equipment ties, control stations | High-pressure small bore | Main headers, power and LNG | Utilities, instrument lines |
Need Help Matching Ends to Your Line Class?
Send FTK Valve your line size, schedule, and pressure class — our engineers will confirm the right end connection for your API 602 forged valves before you order, at no charge.
Answer three questions and the selector below suggests a starting point for your valve end connection selection — the same logic our application engineers use during quotation review.
1. What is the line size?
2. What is the pressure class?
3. How often will the valve need removal?
This selector provides a starting point only. Your piping specification and applicable codes always take precedence.
No. End connections are forged or cast integrally with the valve body and machined in one setup, so a socket weld body cannot be converted to flanged and vice versa. If the piping design changes after your order, the practical options are a new valve or — in limited small-bore cases — a fabricated adapter spool, which adds a weld and a gasket you did not plan for. Confirm the end style against the latest piping isometric before the valve enters production.
An RF flange has a short raised annulus that concentrates bolt load on a smaller gasket area; it is the default for steel industrial piping. A flat face flange is machined flush and is used to mate with brittle components such as cast iron bodies, where a raised face would crack the mating flange during bolt-up. Never bolt an RF valve directly against an FF component without a full-face gasket.
Use a star (criss-cross) pattern in at least three passes — roughly 30%, 70%, then 100% of the target torque — and re-torque after the first thermal cycle, because gaskets creep. Uneven bolt load, not gasket quality, is the most common cause of flange leaks. For critical joints, follow the assembly procedure in ASME PCC-1.
Only within tight limits. Thermal cycling works threads loose over time, so most piping specifications restrict threaded joints to low-pressure, low-temperature utility steam and condensate lines. Where a specification allows them in hotter service, it usually requires the threads to be seal-welded after installation. For main steam headers, specify welded or flanged ends.
Forged body valves built to API 602 are normally offered in four end styles: socket weld, threaded, flanged (RF), and butt weld — selected per your piping specification at order time. Small forged valves are often stocked with SW or threaded ends, while flanged and BW configurations are produced against your schedule and facing requirements. When you request a quotation, state the end style together with the class and material, because it affects lead time.
Order the valve by pipe schedule, not just by NPS — a 6 in Sch 80 valve has a different bore and bevel than a 6 in Sch 40. The valve bore should match the pipe inside diameter closely enough that the full-penetration weld leaves no step in the flow path. If your line transitions between schedules, tell the supplier both schedules so the bevels can be prepared accordingly.
Welded ends, without question — a butt weld has no joint at all in the flow path, and a socket weld’s single fillet is far less sensitive than a thread or a gasket. Threaded joints are the first to weep on compressor and pump skids unless they are seal-welded. If you must use flanged ends near rotating equipment, respect the piping flexibility analysis and re-torque the bolts after commissioning.
A pragmatic approach is to hold flanged spares for valves on equipment ties and control stations, where downtime cost is high, and rely on welded spare bodies only for standard main-line sizes. Replacing a welded-in valve requires hot work, cutting, and fit-up — the spare on the shelf is cheap compared with the outage you will run if it is missing.
Yes. Standard practice per ASME B16.11 calls for a 1/16 in (1.6 mm) gap between the pipe end and the socket shoulder, set before tacking. The gap gives the pipe room to expand axially during thermal cycles; welders who push the pipe hard against the shoulder create a stress-raising joint that can crack the fillet in cyclic service. It is a two-second check that prevents a very expensive repair.
Three things, clearly stated: the end style (RF flange, SW, BW, or threaded); the size, including the pipe schedule for BW or the socket class for SW; and the flange standard and facing if flanged (ASME B16.5 class, or EN 1092-1 PN and type). Add the body material and any testing requirement — for example hydrostatic testing per API 598 — and you will get an accurate quotation in one round instead of three.
There is no single best valve end connection — only the best one for your size, pressure, maintenance strategy, and leak-tolerance requirements. Flanges reward you with serviceability, welded ends reward you with permanent leak-tight integrity, and threaded ends reward you with speed on small-bore lines. If you are specifying forged steel gate, globe, or check valves, FTK (FULL-THINK VALVE) manufactures to API 602 with SW, threaded, RF flanged, and butt weld ends across a full range of pressure classes. Send us your line class and operating conditions, and our engineers will help you confirm the right end connection before you order.
Get the Right Valve Ends the First Time
FTK Valve supplies API 602 forged steel valves in socket weld, threaded, flanged, and butt weld ends — engineered, tested, and shipped from one factory. Tell us your application and receive a quotation with the correct connection specified.
(All images are sourced from the internet. In the event of any copyright infringement, please contact us and we will remove the content promptly.)